Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
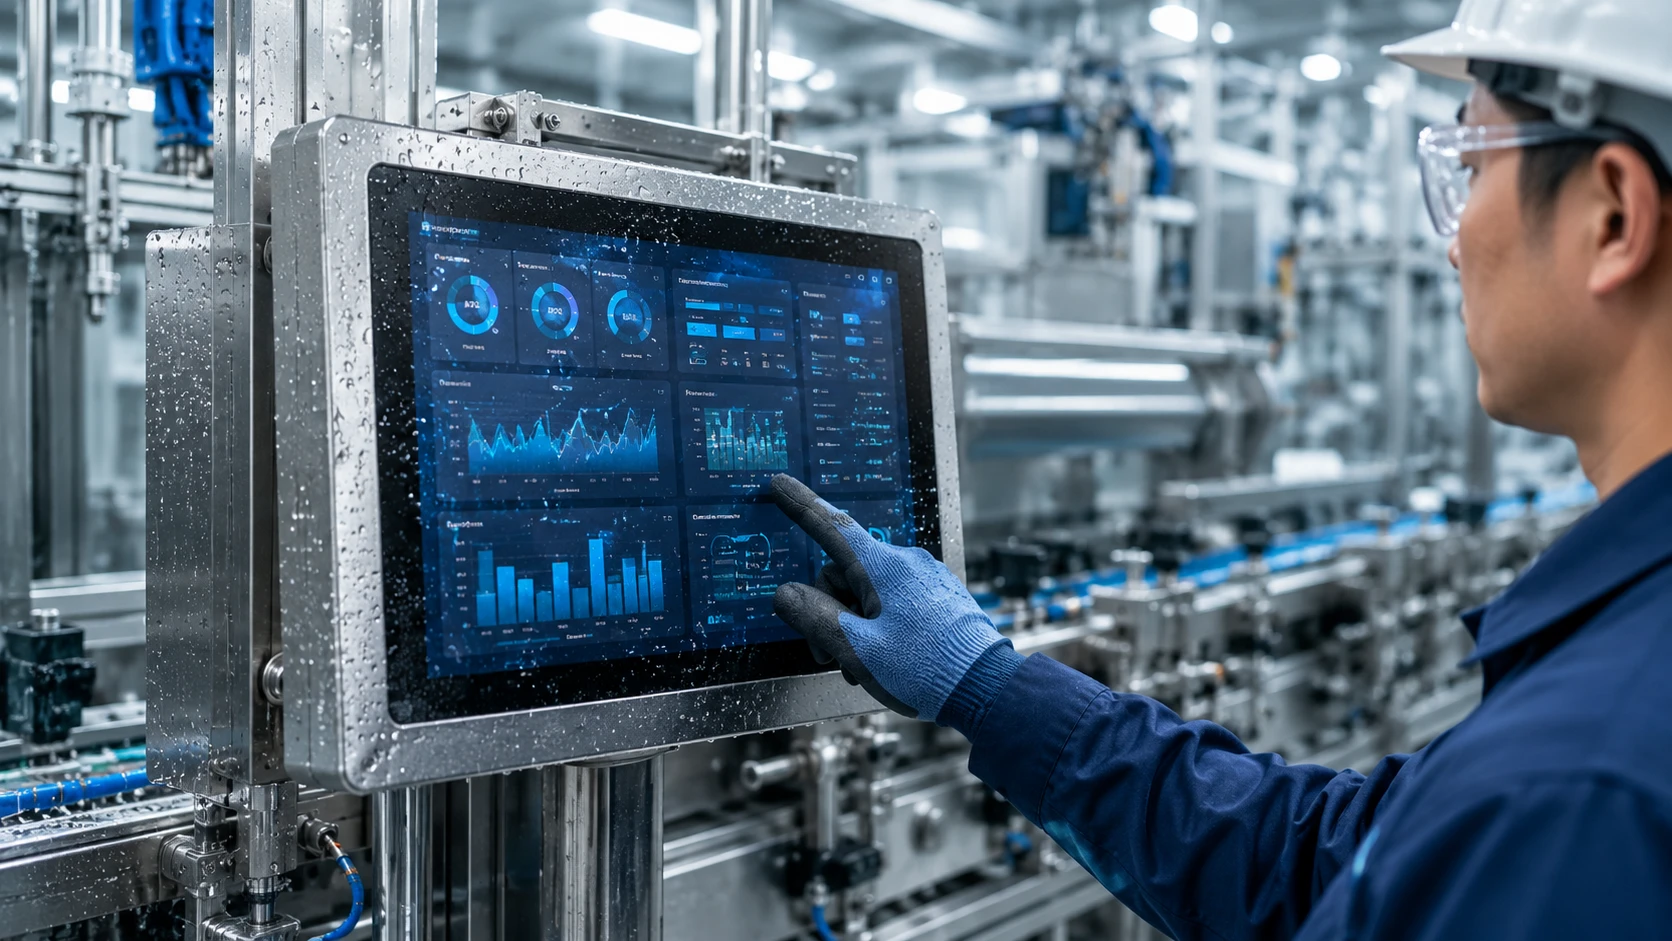
Industrial displays are often deployed in challenging environments where dust, moisture, oil, and continuous operation can significantly impact equipment reliability.
Unlike commercial monitors, industrial displays are specifically designed to withstand harsh conditions while maintaining stable performance. Among the various protection levels available, IP65-rated industrial displays have become one of the most popular choices for industrial automation, manufacturing, transportation, and outdoor applications.
Their sealed design provides excellent protection against dust and water, making them ideal for environments where standard displays would quickly fail.
In this article, we explore the key benefits of IP65 industrial displays and examine the industries and applications where they deliver the greatest value.
IP (Ingress Protection) is an international standard that defines how well a device is protected against solids and liquids.
An IP65 rating consists of two digits:
Protection against solid particles.
Protection against water.
An IP65 industrial display is therefore designed to operate reliably in dusty and wet industrial environments.
Dust is one of the most common causes of industrial equipment failure.
Manufacturing facilities often generate:
These contaminants can damage internal electronic components and reduce equipment lifespan.
IP65 displays utilize sealed front panels and industrial-grade enclosures to prevent dust penetration.
Many industrial environments involve frequent exposure to water, cleaning agents, and humidity.
Examples include:
IP65 protection ensures that water spray and washdown procedures do not affect display performance.
This significantly reduces the risk of equipment downtime caused by moisture damage.
Industrial operations often expose equipment to:
IP65 industrial displays are engineered to withstand these challenges while maintaining reliable performance.
Their rugged design makes them a preferred choice for demanding industrial applications.
Maintenance expenses can be substantial in industrial facilities.
Because IP65 displays are sealed against dust and moisture, they require less frequent cleaning and servicing.
These benefits contribute to a lower total cost of ownership.
For applications operating 24/7, reliability is critical.
IP65 industrial displays help maintain stable performance by protecting sensitive components from environmental hazards.
This makes them suitable for mission-critical systems where downtime is unacceptable.
Many IP65 displays feature industrial-grade touchscreen technology, including:
These features improve durability while maintaining responsive user interaction.
Industrial touchscreens are often designed to support operation with gloves, making them ideal for factory environments.
Industrial displays serve as Human-Machine Interfaces (HMIs) for:
IP65 protection ensures reliable operation on the factory floor.
Food production environments require frequent washdowns and strict hygiene standards.
IP65 displays are commonly used in:
Their waterproof design helps maintain compliance with sanitation requirements.
Pharmaceutical facilities demand clean and controlled environments.
IP65 industrial displays support:
Their sealed design helps reduce contamination risks.
Transportation applications often expose equipment to outdoor conditions.
Examples include:
IP65 protection improves long-term reliability in these environments.
Outdoor equipment must withstand:
IP65 industrial displays are frequently used in:
Their rugged construction supports reliable outdoor operation.
Modern logistics centers utilize industrial displays for:
IP65 displays help ensure dependable performance in busy warehouse environments.
When selecting an IP65 industrial monitor, consider the following features:
Provides:
Choose between:
Based on your operational requirements.
Fanless systems offer:
Suitable for:
Common mounting methods include:
Industry 4.0 technologies require reliable human-machine interfaces capable of operating continuously in demanding environments.
IP65 industrial displays support:
Their durability and reliability make them a key component of modern industrial infrastructure.
IP65 industrial displays offer exceptional protection against dust and water while delivering the reliability required for industrial automation and smart manufacturing applications.
From factory floors and food processing plants to transportation systems and outdoor installations, IP65-rated displays help reduce downtime, lower maintenance costs, and improve operational efficiency.
As industrial environments become increasingly connected and automated, demand for rugged IP65 industrial displays will continue to grow.

