Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
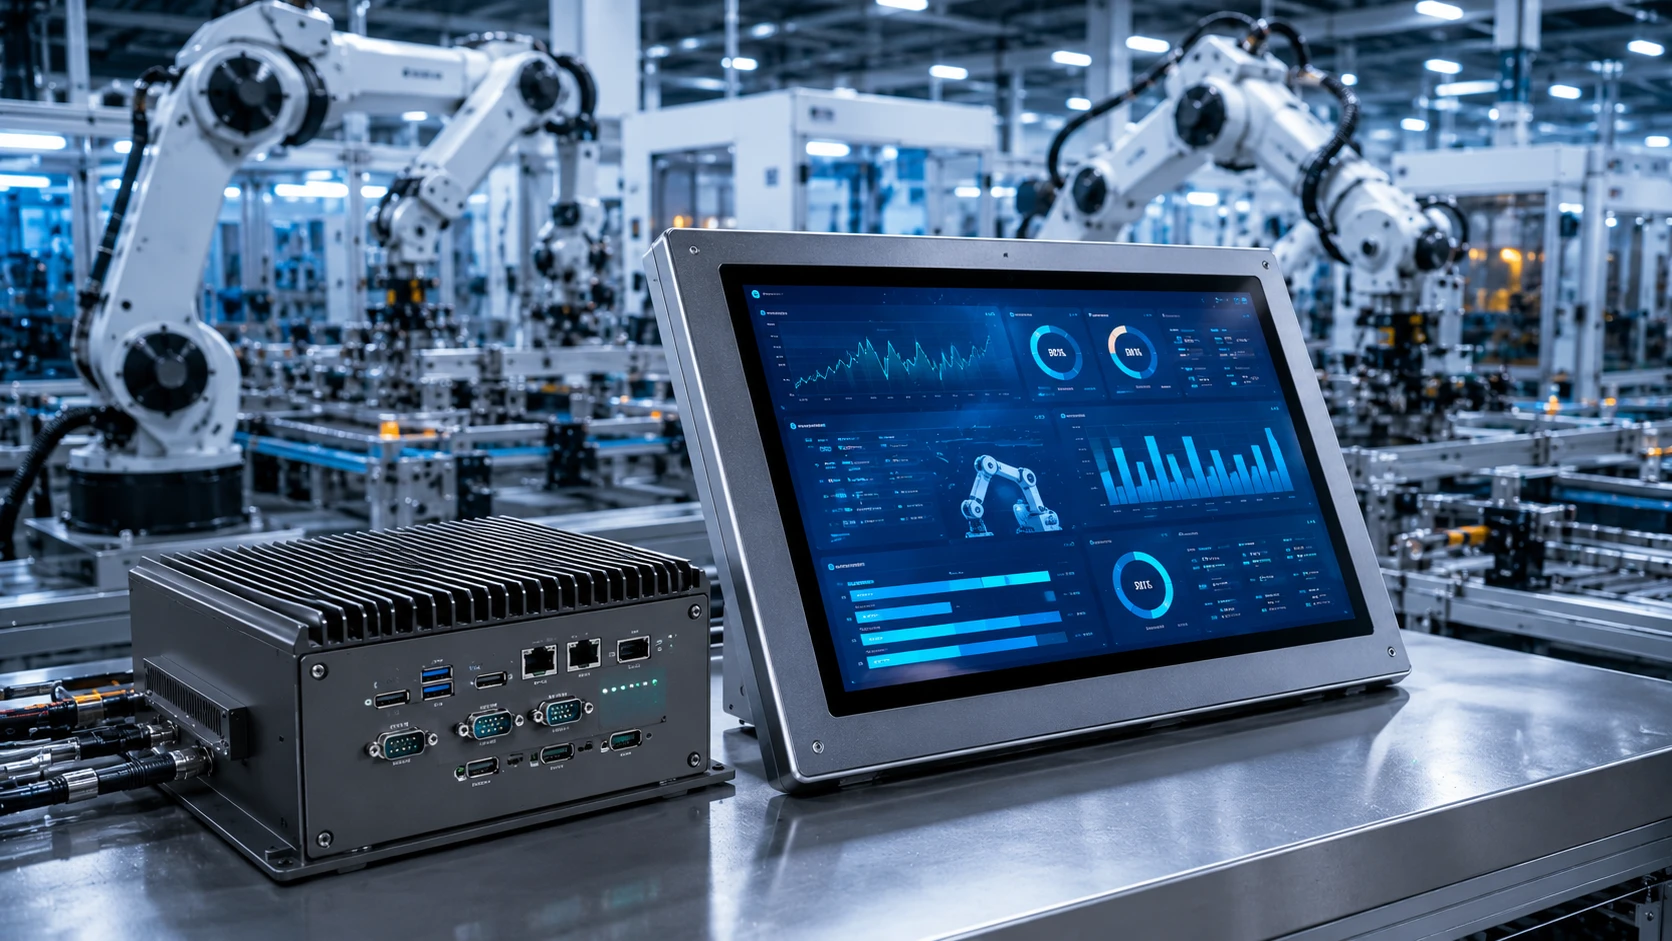
Factory automation has become a key driver of productivity, quality, and competitiveness in modern manufacturing. As companies continue to embrace Industry 4.0 technologies, the demand for reliable and high-performance industrial computing solutions is rapidly increasing.
Industrial computers play a critical role in connecting machines, collecting data, controlling production processes, and enabling real-time decision-making. Unlike commercial PCs, industrial computers are specifically designed to operate in harsh environments while maintaining long-term stability and reliability.
From automated production lines to intelligent quality inspection systems, industrial computers are helping manufacturers improve operational efficiency and reduce production costs.
In this article, we explore how industrial computers contribute to factory automation and why they have become essential components of smart manufacturing systems.
An industrial computer (Industrial PC or IPC) is a rugged computing platform designed for industrial environments.
Industrial computers typically feature:
These characteristics make industrial computers suitable for continuous operation in demanding factory environments.
Industrial computers act as the central processing unit of many automation systems.
They are responsible for:
By integrating these functions into a single platform, industrial computers improve efficiency across the entire production process.
Modern manufacturing facilities generate enormous amounts of data every second.
Industrial computers collect information from:
This data can be processed in real time to support operational decisions.
Real-time data analysis enables manufacturers to identify inefficiencies before they impact production.
Factory automation relies on seamless communication between machines.
Industrial computers support multiple industrial protocols such as:
These communication capabilities enable different systems to exchange information quickly and reliably.
Industrial Panel PCs and industrial displays provide operators with intuitive interfaces for monitoring and controlling production systems.
Modern HMI solutions allow operators to:
User-friendly interfaces help simplify complex industrial processes.
Unexpected equipment failures can result in significant production losses.
Industrial computers support predictive maintenance strategies by continuously monitoring machine conditions.
Typical monitoring parameters include:
Predictive maintenance helps manufacturers address issues before failures occur.
Industrial Internet of Things (IIoT) technologies connect factory equipment to intelligent monitoring systems.
Industrial computers serve as edge devices that collect and process data locally before sending it to cloud platforms.
IIoT integration enables manufacturers to achieve higher levels of automation and visibility.
Many factory applications require immediate responses.
Sending all data to the cloud can introduce latency.
Industrial computers perform edge computing tasks by processing data directly at the production site.
Applications include:
Edge computing has become a critical component of Industry 4.0 strategies.
Automation systems depend on precise control and monitoring.
Industrial computers help maintain consistency by:
Accurate production processes directly impact profitability.
Machine vision is widely used in modern manufacturing for:
Industrial computers process image data from cameras and perform real-time analysis.
Machine vision systems significantly improve production accuracy and speed.
Many manufacturing facilities operate around the clock.
Industrial computers are designed for:
Their robust construction helps minimize system failures.
Reliable operation is essential for high-volume manufacturing environments.
Industry 4.0 requires intelligent computing platforms capable of connecting people, machines, and data.
Industrial computers support:
These technologies enable manufacturers to optimize production and remain competitive in a rapidly changing market.
Industrial computers are widely used in:
When selecting an industrial computer, consider:
Choosing the correct platform ensures long-term operational success.
Industrial computers have become the backbone of modern factory automation systems.
By enabling real-time data processing, machine communication, predictive maintenance, edge computing, and Industrial IoT integration, they help manufacturers improve efficiency, reduce costs, and increase productivity.
As smart manufacturing continues to evolve, industrial computers will remain essential for building more connected, intelligent, and efficient factories.

